Where the tooling charge goes
On a rigid board, the non-recurring cost is mostly drill and rout programming. On a flex or rigid-flex board it is a list:
- Coverlay tooling — the openings have to be cut in a film that will move during lamination.
- Stiffener tooling — PI, PET, FR-4 or stainless steel outlines, cut separately and bonded.
- Outline tooling — laser or route for prototypes, a steel rule die for volume.
- Test fixture — flying probe for low volume, a hard-wired fixture when volume justifies it.
- Carrier or panel frame — a thin flex panel needs support to survive SMT and reflow.
Each item has its own break-even, which is why a flex quotation can look unreasonable at ten pieces and competitive at ten thousand.
Prototype and volume are different processes
At low volume, laser cutting and routing keep the tooling cheap and let the design change without scrapping a die. At volume, a steel rule die or a matched punch and die set cuts parts far faster, and a hard-wired test fixture replaces the flying probe; both add upfront cost and both reduce unit price.
The design decision that follows is not "which is cheaper" but "how many pieces before the die is paid for". A part that will never exceed a few hundred units should stay on laser cutting even if the unit price is higher.
Rigid-flex adds steps, not just tools
A rigid-flex board is a flex core laminated between FR-4 sections, with the flex areas cleared of stiffener and prepreg. That means more lamination control, more registration steps, and a carrier to hold the flex tails flat through assembly. The tooling reflects those steps: the flex core is tooled like a flex, the rigid sections like a rigid board, and the two have to register with each other.
Panel utilisation is part of the cost
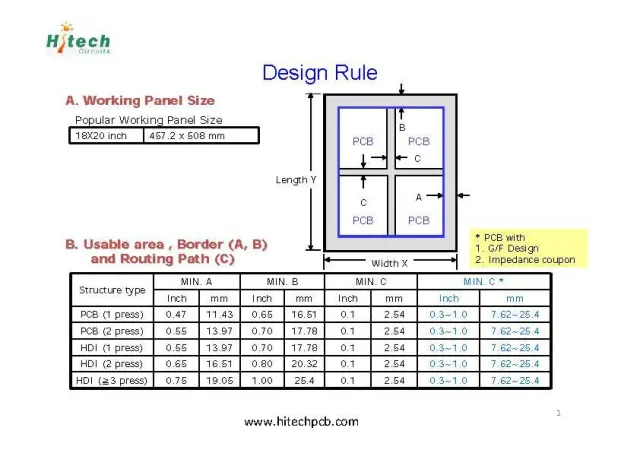
Flex panels are limited to 9.842″ × 19.685″ and the parts are usually small, so a well-planned array matters as much as the die. A layout that leaves large dead areas on the panel pays for them in every lot, long after the tooling is amortised.
How to compare the options
Put the whole assembly on one line: board cost, connectors, cable, assembly labour, test and expected field failures. Rigid-flex tends to win where a connector would have been needed anyway and the housing is tight; a separate flex plus connector tends to win where the boards are large and the connection is simple.
Ranges for both constructions are on the flexible PCB page and the rigid-flex page; the capability page lists the process limits behind the tooling decisions.