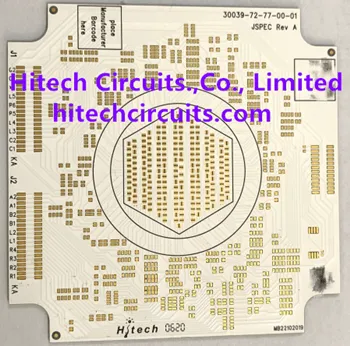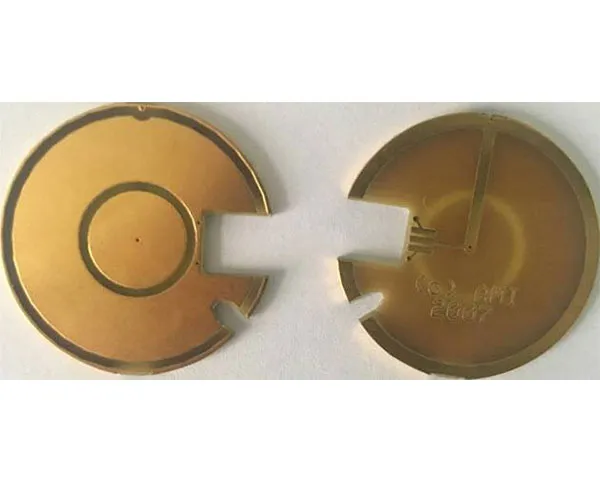
An aluminium or metal-core board carries the circuit on a thermally conductive dielectric bonded to a metal base. The heat path runs straight down through the base instead of sideways through the copper, which is why lighting, power and motor-drive designs use it: the board itself is the heat sink.
Why a metal base instead of FR-4
- Thermal path — heat spreads through the base under every hot component, so LED pads, MOSFETs and shunt resistors do not need a separate aluminium heat sink bolted underneath.
- Mechanical rigidity — a metal core resists bending at long and thin shapes where FR-4 would need stiffeners.
- Current capacity — copper from 18 µm to 240 µm carries the load of a driver or power stage without widening the layout.
- Dimensionally stable — warp and twist stay below 0.5 mm across the 5 × 5 mm to 1900 × 480 mm size range.
Constructions built here
Single-sided MCPCB with a punched or routed outline, double-sided and 2 to 4 layer metal-core boards, COB MCPCB for chip-on-board LED arrays, and copper-base boards where aluminium is not thermally conductive enough. Driver and control sections that need more density are built on FR-4 up to 38 layers and produced in the same order as the metal-core part.
What the process holds
Minimum trace width and spacing are 0.1 mm with hole position tolerance of ±0.075 mm, so the LED pitch and the connection to the rest of the fixture are fixed before panelisation. Drilled holes start at 0.2 mm, punched holes at 1.0 mm, and square slots from 0.8 × 0.8 mm are punched in the same pass as the outline. Hole wall copper runs 18–40 µm, silk print and component marking hold ±0.075 mm, and the smallest component mark is 0.15 mm.
Assembly and inspection
LED reels, connectors and terminals are placed on four SMT lines running six million chips per day and three DIP lines handling 1.6 million through-hole pieces per day, with reflow profiles set for the thicker thermal mass of a metal-core panel. X-ray inspection covers joints under connector bodies, and cable, harness and box build follow in the same plant, so a finished luminaire or power unit can leave as an assembled product. Lighting programmes are covered in more detail on the LED lighting page, and automotive metal-core work under automotive PCBs.
Getting a quotation
Send the Gerber set with the base type, board thickness, copper weight, surface finish and quantity — plus the LED type and drive current where lighting is involved. Prototypes come back in 1–3 days and medium volume in 4–10 days; the capability page lists the process limits behind the quotation, and certificates are on the certifications page.
Where the metal-core panels continue into assembly, the China PCB assembly page covers SMT, through-hole, sourcing and box build in the same Shenzhen plant.