Four gates, not one final inspection
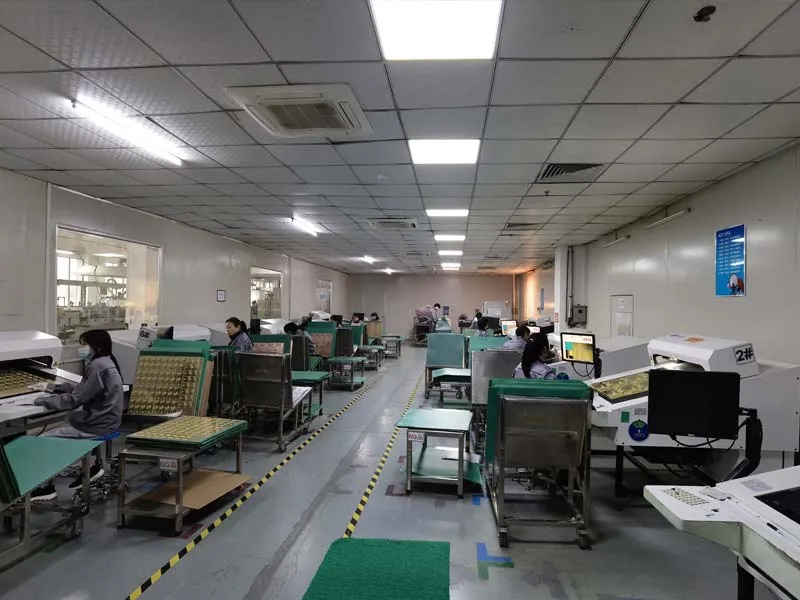
Testing a batch at the end of the line only tells you how many boards are already scrap. Quality is therefore built into four gates:
- IQC — incoming quality control. Components and bare boards are checked on arrival, before they can reach a feeder. A wrong reel caught here costs a phone call; the same reel caught after reflow costs a lot.
- IPQC — in-process quality control. Each process is inspected as it runs, so a printing or placement problem is corrected within the lot rather than after the whole batch has been assembled.
- QC — test and inspection. The finished assembly is tested and inspected, with a first article inspection on every process and workmanship judged against IPC-A-610.
- QA — final quality assurance. A sample inspection plan releases the lot, reviewing the records from the gates behind it.
Inspection along the line
Optical and X-ray inspection cover what the eye cannot reach. Solder paste inspection runs before placement, checking volume and alignment; automated optical inspection runs after reflow, catching missing, offset and tombstoned parts; X-ray inspection looks at the joints hidden under BGA, QFN and other area-array packages, including voiding and bridging that no optical check can see.
Ionic contamination is measured by ionograph down to ppm per square centimetre — the residues that pass every electrical test on the day of assembly and cause electrochemical failure months later in the field.
Electrical and functional test
In-circuit test drives the assembled board through a bed-of-nails fixture, checking component presence, value and orientation as well as opens and shorts. Flying probe does the same job without a fixture, which suits prototypes and small batches where the fixture cost would not be recovered; a manufacturing defect analyser narrows failed boards down to opens, shorts, missing or reversed parts.
Functional test is where the product is proved to work: the assembly is exercised on a fixture built to the customer's test points and test steps, with the acceptance criteria taken from the customer procedure. Firmware is loaded and the product configured as part of the same stage, so a board that leaves test is a working unit.
Reliability testing
Where the application demands it — automotive, medical, industrial and outdoor products in particular — boards go through burn-in, thermal cycling, hi-pot and vibration testing alongside reliability checks on the process itself. These are run alongside, not instead of, the inspection gates: a product can pass every electrical test and still fail a thermal cycle, and the point of running both is to find that out before the customer does.
Specifying the test with the build
Test requirements are easier to agree before assembly than after. Send the test points, the test steps and the pass criteria with the Gerber set and the BOM, and the fixture, the program and the acceptance limits are prepared alongside the build; where only a functional description exists, the DFT review works out what the tester has to reach and what failures the product actually produces.
Boards are held to IPC-A-610 workmanship, and the plants behind them are certified to ISO 9001:2015, IATF 16949:2016 and ISO 13485:2016 for automotive and medical programs — see the certifications page for the issued certificates, and the capability page for the process limits the inspection plan is built against.