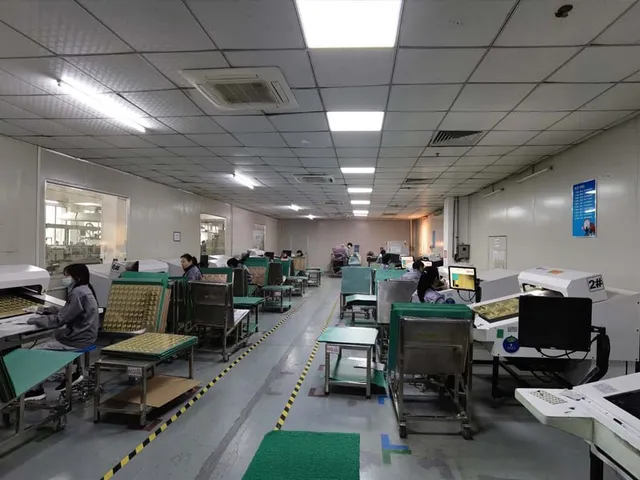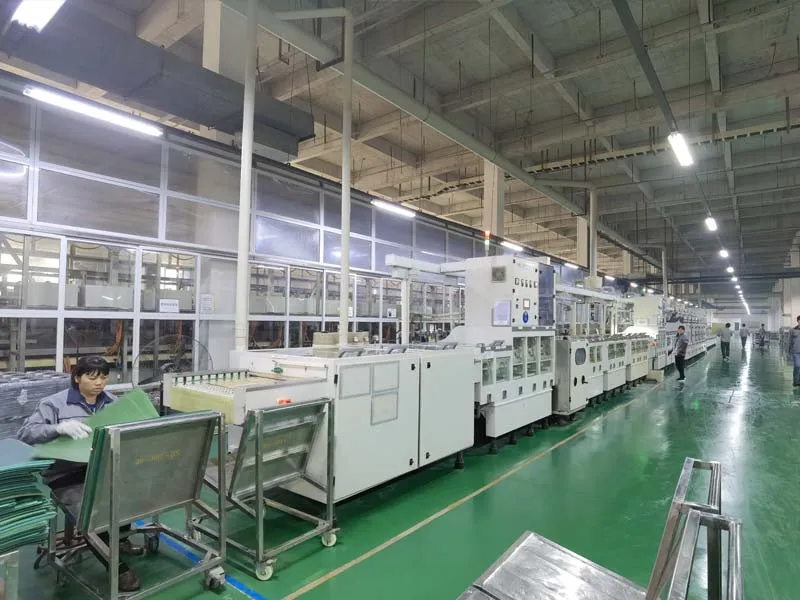
One floor, from prototype to volume
Volume is a batch size, not a different process. The placement programs, stencil design, AOI recipes and X-ray settings signed off on the first boards are the ones the production run uses, which is why the same four SMT lines and three DIP lines take both a fifty-piece batch and a mass-production order — and why a design that behaved on the prototype behaves in the field.
Three commercial models run on those lines:
- Full turnkey — the Gerber set and the BOM are all that is needed; parts are sourced, boards fabricated, assembled, tested and packed.
- Partial turnkey — the customer supplies the bare boards, or selected critical components, and everything else is bought and built here.
- Consignment — the customer supplies the components; assembly, inspection and test stay with us.
Components are bought by the sourcing team against the whole BOM, so a high-mix order does not turn into a list of minimum-order charges and separate freight bills.
Engineering review before production
Design for manufacturing (DFM) checks the customer's own documents — Gerber files, bill of materials, assembly drawings and circuit diagrams — for anything that would slow the line or lower the yield. Panelisation is designed, the component list is verified before parts are ordered, and a solder mask thickness is recommended for the output rate the design needs.
Design for testing (DFT) covers the other half: where test points should sit, which probe types and fixtures the test needs, what the tester can reach, and whether the test procedure detects the failures the product actually suffers. Both reviews run before the first article, not after the first failed lot.
What the floor holds
Capacity is four SMT lines placing six million chips per day down to 01005 and 0201 packages at 4 mil (0.1 mm) pitch, on one or both sides of the board, plus three DIP lines handling 1.6 million through-hole pieces per day. Stencils are cut on site within four hours; prototypes come back in 1–3 days and medium volume in 4–10 days, with mass-production timing set by the BOM and the component lead times inside it.
Inspection follows the board along the line — SPI before placement, AOI after reflow, X-ray for BGA and QFN joints — then in-circuit or flying probe test and functional test against the customer's procedure. Rework, including BGA rework and re-balling, is done in-house and verified by X-ray rather than being returned to the customer.
Getting a volume quotation
Send the Gerber set, the BOM with manufacturer part numbers, the pick-and-place file, the quantity and the required schedule. BOM quotations are issued within 24 hours; the process limits used for that quotation are on the capability page, and the issued certificates on the certifications page.