Material and lay-up
The build starts with a decision about where the copper comes from. Where the weight exists as foil, the laminate is ordered with heavy copper on the layers that need it; where the design needs more, the balance is plated during the build. Heavy foil arrives with its own handling rules: it does not drape or conform the way thin foil does, and the prepreg has to fill a deeper step around every heavy area.
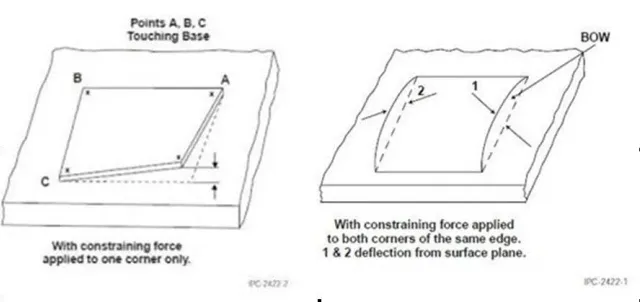
Copper balance is decided here as much as in layout. A stack-up with heavy copper on one side and none on the other bows during lamination, so heavy areas are mirrored where the design allows, and the remainders are absorbed by the process.
Drilling
Thicker panels are heavier, and a heavy copper layer is harder on the drill. Bit consumption rises, entry and exit material is chosen for the extra load, and the hole diameter stays inside the published limits: 0.15 mm mechanically, 0.1 mm by laser, with a 15:1 aspect ratio for the plated barrel.
Plating
Plating is where the thickness is built. Heavy copper often needs several cycles rather than one long pass, because a single pass at the current density required for the target thickness would burn the resist and plate unevenly across the panel. Pattern plating deposits copper into the circuit rather than across the whole surface, which is both cheaper in copper and better for flatness.
Imaging and etching
Etching a heavy layer takes more than one pass. Removing 700 µm of copper in a single pass would undercut the resist badly and leave a trapezoidal trace far narrower than drawn, so the panel is etched in stages with the etchant refreshed between them. This is why the minimum line and space on a heavy layer is quoted against its weight: the process, not the artwork, sets the limit.
Mask, legend and finish
Solder mask is printed twice over heavy copper. The first print covers most of the step; the second closes the thin areas at the shoulders of the traces and the air pockets at the edges, and builds enough film to survive assembly. Legend follows the same surface, which is why character legibility on a heavy board is checked rather than assumed.
Surface finish is chosen after the geometry: HASL follows the copper contour, ENIG and immersion tin give a flat pad for fine-pitch parts, and flash gold suits connector edges.
Test and inspection
Boards run through 100 % electrical test, AOI where the surface allows it, X-ray where joints or inner layers are hidden, and cross-section on the coupon for hole-wall and surface copper. Acceptance is against IPC-6012B for fabrication and IPC-A-600H for the workmanship, with UL recognition under E354070. Heavy copper joints that will be assembled are reviewed with the reflow profile in mind, since the copper carries heat away from the pad.
Where the sequence is agreed
The fabrication sequence is fixed by the stack-up, so it is settled in DFM before tooling. The published range is on the heavy copper PCB page, the design consequences in the design guide, and assembly of the finished board on the PCB assembly page.